 ☰ Menu
On-line moisture measurement is the measurement of choice for many industries. Understanding how on-line moisture measurement works in comparison with other moisture measurement methods will quickly shed light on why it is, often, the best method for accurate measurement.
When making a laboratory moisture measurement, you must first assign laboratory personnel to periodically visit the process line to gather product samples. The personnel must be fully clothed in the necessary PPE, collect samples in approved sample containers, seal properly, and transport back to the lab for the test to begin. The test itself is a complex process that involves the following steps:
Be sure that sample size, oven temperature, and drying time are appropriate for each product or formulation
After the test is completed, the moisture percentage is then communicated to the process operator so the appropriate temperature/line speed changes can be made to achieve the target moisture level. The above process then must be repeated every 15 to 30 minutes for the duration of every shift.
Compare that process with a handheld moisture measurement which requires the training and assignment of plant personnel to use the portable moisture meter. Then, clothed in appropriate PPE, they must visit the process line periodically and place the correctly-calibrated, handheld moisture meter on the processed product. From there, the moisture content measured must be reported to the process operator so the necessary changes can be made. Similar to lab measurements, the process must be repeated every 15-30 minutes to ensure that the moisture limits are being achieved. Furthermore, records must be maintained of each test for production reports.
Finna Sensors is the global leader in detecting moisture in lumber – offering the most highly-adopted end-to-end solution in the industry.
Learn MoreNow, let’s compare those first two measurement methods to utilizing an on-line moisture meter to receive and adjust in real-time.
First, you must calibrate the on-line, continuous NIR moisture meter. The calibration only needs to happen once. Then, you place the readout console or digital display where the operator can see continuous moisture results. Adjustments can be made as soon as an unwanted change in the process line occurs. The built-in reporting package with Finna Sensors NIR solutions creates and maintains production records for you.
There’s no need for lab or process personnel to gather samples, vastly decreasing risk of staff injury. No need for expensive lab equipment or chemicals, no utility costs for heating ovens to high temperatures for extended periods of time. All of these things save on operating costs and overall budget, but these advantages only skim the surface.
The OMNIR On-Line Near Infrared Moisture Sensor not only delivers accurate data instantaneously and non-destructively, it also monitors its own health to help keep your operation running smoothly. See how Finna Sensors can assist in augmenting your process.
Learn MoreThe real benefit of on-line moisture meters comes from eliminating the possibility of out-of-spec product occurring between lab samples. A constant, controlled, set-point moisture measurement improves product quality across the board. In addition, it reduces or eliminates:
To put it simply, NIR on-line moisture measurement can revolutionize your entire operation.
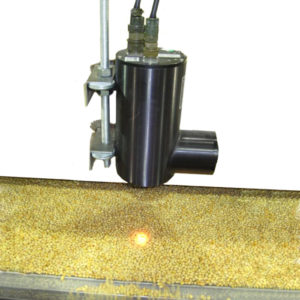 The SMART III Near Infrared (NIR) moisture sensor provides continuous, instantaneous and non-destructive moisture measurements. Process outputs are available to provide automatic moisture control and data logging.
Key Features
Ideal in these industries:
Ag/Food Processing · Biomass · Building Materials · Chemical/Pharmaceuticals · Mineral/Mining · Pulp & Paper · Textiles
From conveyors & webs to chutes & silos, we offer a solution to meet your needs.
Learn MoreCopyright Finna Sensors 2026
 Cart


 by Webolutions